
近日,福斯达为赤峰广钢气体金通二期项目提供工艺包及核心冷箱设备的 KNONAr-44000 空分装置传来捷报:装置顺利完成全流程调试,实现一次开车成功并稳定达产。凭借优异的运行表现,项目团队收到客户发来的感谢信,获高度认可。
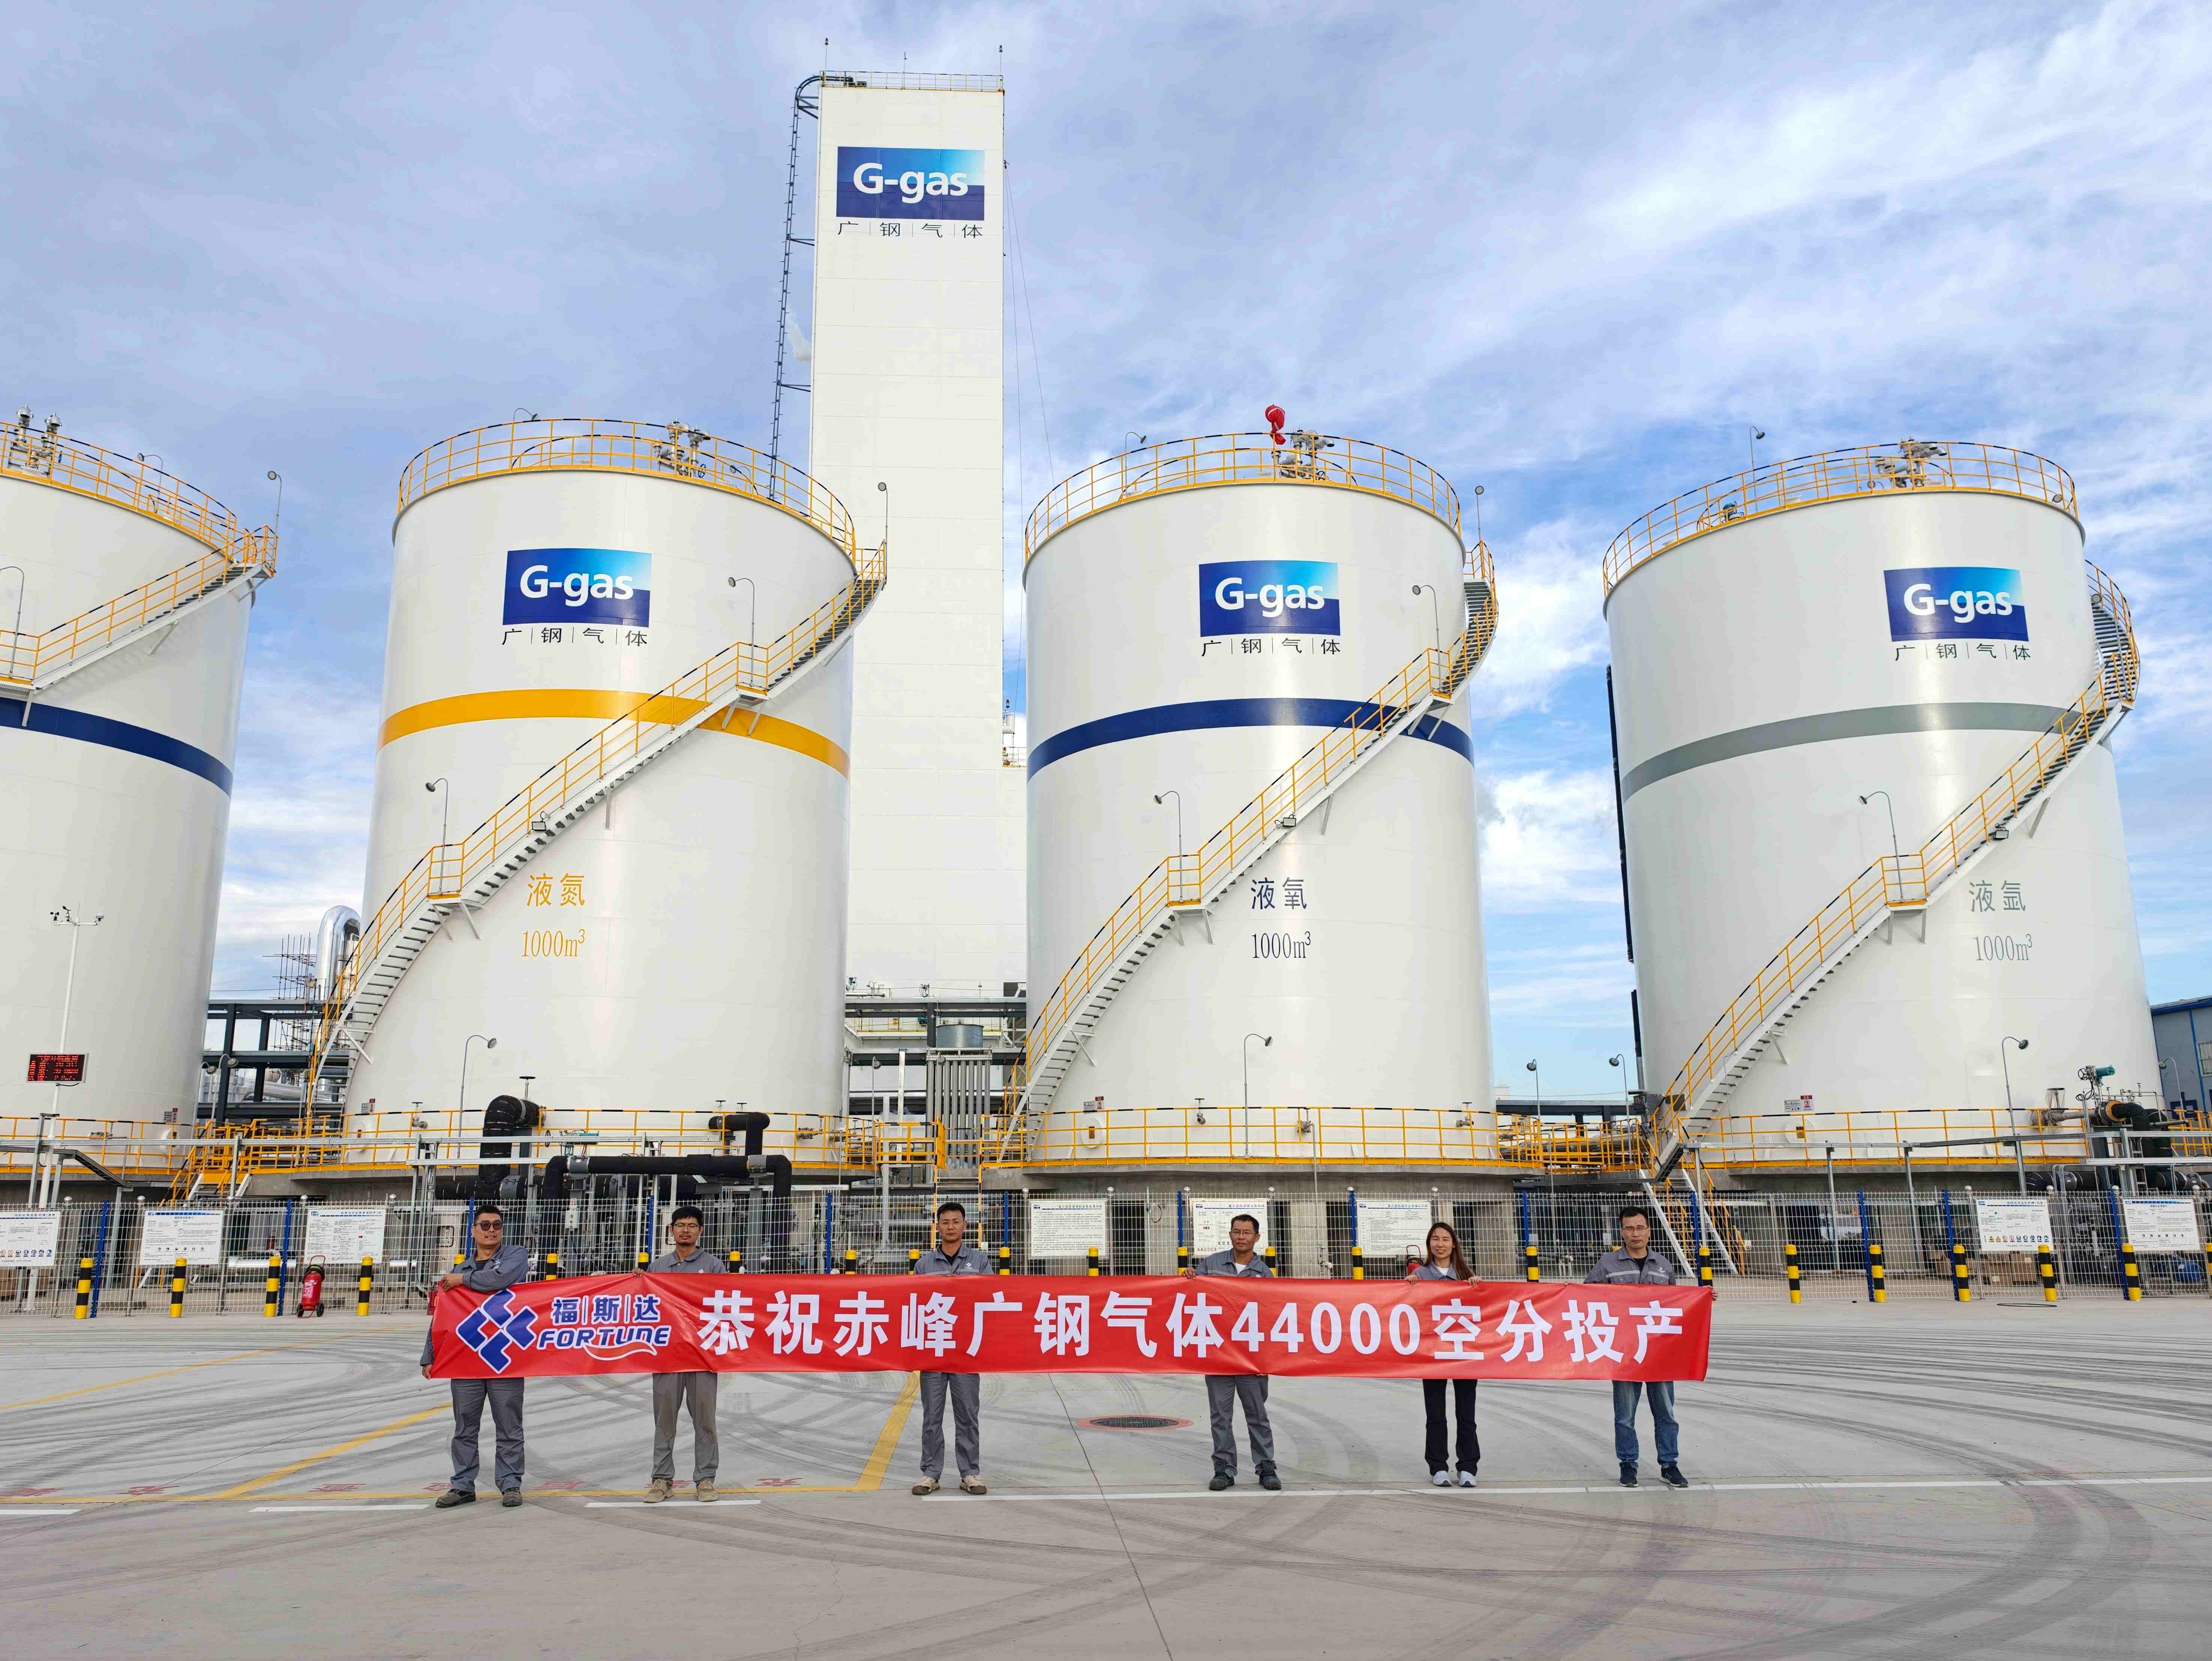
本套装置设计气态氧产能44000Nm³/h,可同步产出氧、氮、氩多品类高纯工业气体,充分适配大型工业气体园区大规模、多品种供气需求。从工艺方案论证、核心冷箱智造到整机性能校验,项目全流程执行严苛质量管控,为装置长周期稳定、高效运行筑牢根基。
依托深厚的深冷技术积淀,本次装置无需传统裸冷工序即可一次开车达产,大幅压缩现场调试周期,充分验证了福斯达顶尖的设备制造精度与工艺设计能力。投产后装置氩气产量稳定超产,各项运行指标均优于设计值,切实为客户提升运营效益。
项目实施期间,福斯达专项技术团队全程驻场协同,高效联动多方参建单位,快速响应现场各类技术需求。扎实的技术支撑、可靠的产品品质与务实的现场服务,赢得了业主及参建各方的一致好评。
本次项目的顺利投产,是福斯达深耕大型空分装备领域、以品质赢取市场信赖的又一标杆成果。未来,福斯达将持续深耕气体分离核心技术,迭代升级大型空分系统性能与全周期服务能力,为全球客户提供稳定可靠的一体化深冷与油气解决方案。
Good News | Fortune’s GOX44,000 ASU Achieves One-Time Startup
In recent days, the GOX44,000 air separation unit supplied by Fortune for Chifeng Guanggang Gas Jintong Phase II project achieved one-time successful startup and stable full-load operation. The outstanding performance earned an official thank-you letter from the client.
Designed with an oxygen capacity of 44,000 Nm³/h, the unit can produce high-purity oxygen, nitrogen and argon to meet large and diversified gas demands of industrial gas parks.
Benefiting from precise cold box design, the unit reached full load smoothly without conventional bare cooling. Our on-site technical team provided timely and professional support throughout the project.
This project demonstrates Fortune’s solid capability in large cryogenic air separation equipment. We will keep optimizing gas separation technologies and supply trusted integrated cryogenic solutions for industrial partners worldwide.


